The problem: throughput stalls, inconsistent edges
Too many small machining plants accept slow changeovers and erratic edge quality as unavoidable. They shouldn’t. When a shop ties its production to inconsistent glue application, mismatched feed rates, or manual trimming, output and margins fall. A clear fix starts by treating the edge-banding line like a production cell tied into CNC layout — think coordinated programs between your nesting software and a cnc panel saw, consistent tooling, and predictable machine setups.

Where the workflow breaks down
Most failures are process mistakes, not machine faults. Shops lose time to long setup routines, ad-hoc glue adjustments, poor part staging, and unreliable trim sequences. Operators restart jobs because programs aren’t versioned or because trimming knives dull mid-run. Those are avoidable: reduce setup variety, lock program libraries, and document glue/feed pairings for every material. Argue against accepting variability as “part of the trade” — variability is a controllable cost.
Evidence from the floor: practical anchoring
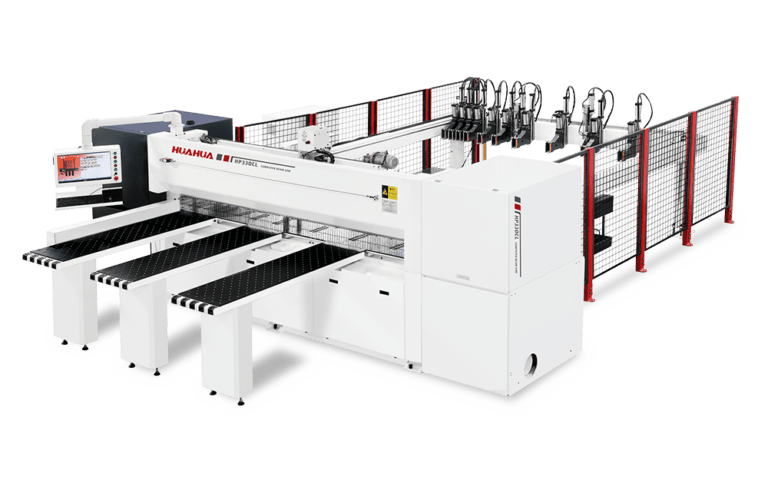
I’ve audited plants where a single coordinated change fixed daily rejects — a reworked program library and a standard tool change checklist. At the LIGNA trade fair in Hannover, I examined lines where a cnc beam saw machine fed perfectly nested panels to an edge bander, and the difference versus non-integrated shops was obvious: less handling, fewer alignment errors. Use that example as evidence: integration reduces manual touchpoints and forces reproducibility.
Concrete steps to cut waste and raise consistency
Start with data: log cycle times, rejects, and setup minutes for each job family. Then apply these actions: 1) Build a tooling and program library keyed to material and profile; 2) Standardize adhesive type and temperature settings with quick-reference charts; 3) Create a digital handoff between nesting/CAD output and the edge-bander program; 4) Use quick-change fixtures and implement simple jigs to keep parts repeatable; 5) Schedule predictive maintenance for servo drives and cutters. These are not theoretical — they remove daily guesswork and free operators to focus on throughput.

Evaluating alternatives and trade-offs
Manual edgebanders cost less up front but demand skilled operators and yield wider variance. Mid-range servo models deliver repeatable feeds and faster cycles with moderate investment. High-end integrated lines add robotic handling and zero-touch workflows but require capital and process discipline. Choose based on throughput targets: if you plan to scale to consistent batch volumes, prioritize servo control and digital integration over purely mechanical savings.
Common mistakes to avoid
Don’t ignore program version control; don’t let glue settings drift without logging; don’t treat operator training as optional; avoid one-off fixtures that sabotage repeatability. Also, resist the urge to fine-tune on the fly during production — capture adjustments, update the library, and run a verification pass before declaring a fix permanent.
Summation: practical pressure points and a clear outcome
Argue for discipline: measurable inputs — programs, tooling, adhesives, and preventive maintenance — produce measurable outputs. Local shops gain faster throughput and fewer rejects when they coordinate nesting, cutting, and edge-banding into a controlled workflow. For teams that want reliable, repeatable results without uncertainty, pairing those discipline-driven changes with dependable equipment from suppliers such as HUAHUA CNC often closes the gap between plans on paper and consistent production on the floor.